
When operating the KD-MJQ-2 on a busy factory floor, the immediate difference is the striking absence of screeching drill bits, airborne metallic dust, and messy shavings. Instead, operators experience a smooth, controlled actuation followed by a decisive, rhythmic thud as the hydraulic system drives the rivet through solid metal. This industrial self-piercing riveting machine is engineered specifically for busduct housing clinching, transforming a traditionally labor-intensive, multi-step task into a rapid, fluid motion. The equipment delivers a permanent, visually clean mechanical interlock without generating heat-affected zones, thereby preserving the structural integrity and protective coatings of the metal panels. The finished joint leaves a flush, aesthetically pleasing surface on the top sheet and a clean, snag-free button on the underside, ideal for densely packed electrical transit systems where internal clearance is critical.
By completely eliminating the need for pre-drilling, hole deburring, or precise manual alignment, this equipment drastically compresses the overall assembly cycle of complex busduct enclosures. A single rivet achieves a fully formed, secure joint in mere seconds. Production managers will notice an immediate acceleration in daily output, allowing assembly lines to process significantly larger volumes of electrical transit systems within the exact same operational shift, effectively multiplying workforce productivity.
Designed from the ground up to conquer demanding industrial fastening requirements, the system effortlessly handles the specified 1.5mm + 1.5mm iron thickness. The resulting cold-formed joint exhibits exceptional shear and tensile strength, which is absolutely crucial for heavy-duty electrical housings that must withstand constant environmental stress, transit vibrations, and internal component weight. It also adapts remarkably well to various composite metal combinations frequently utilized in modern, customized electrical infrastructure projects.
The highly intuitive, one-button actuation significantly lowers the technical threshold for floor operators, reducing reliance on specialized labor. Because the machine automatically pierces and clinches the panels in a single, continuous stroke, workers do not need to spend exhausting hours on meticulous manual alignment. This streamlined, ergonomic operation directly reduces initial training periods, minimizes operator fatigue, and drastically lowers the risk of human error, ensuring consistent joint integrity across thousands of successive cycles.
Operational flexibility remains a core advantage of this riveting setup. The precision-machined tooling accommodates multiple standard specifications of self-piercing rivets (SPR). Whether a specific production run requires minor adjustments for slightly different panel densities, varying coating thicknesses, or specific joint strength profiles, the adaptable die and punch configuration ensures continuous operation. This means facilities can handle diverse product lines without the need for purchasing entirely new fastening machinery.
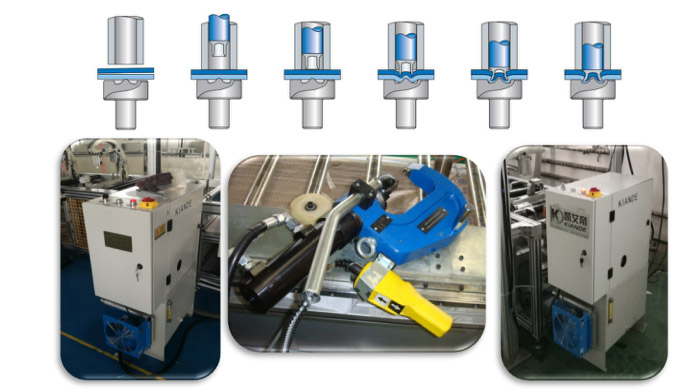
Understanding the technical parameters is crucial for integrating this machinery into demanding production environments. The steady, low-frequency hum of the 380VAC 4.5kW motor signifies a power plant built for endurance. When the trigger is engaged, the tactile feedback is immediate and controlled. The formidable 25MPa maximum pressure guarantees that the specified 1.5mm + 1.5mm iron sheets are permanently fused, creating a mechanical interlock that resists vibration and thermal expansion. A massive 50-liter oil tank capacity acts as a thermal buffer; it ensures the hydraulic fluid remains at an optimal viscosity, preventing overheating and maintaining consistent pressure even during relentless, multi-shift operations. Furthermore, the inclusion of a 10000mm (10-meter) oil pipe provides an exceptionally large working radius. Operators can effortlessly maneuver the clinching gun around bulky, oversized busduct segments, eliminating the dangerous and time-consuming need to constantly reposition the heavy main power unit via cranes or forklifts. The generous 50mm gun head stroke offers ample clearance, allowing the tool to navigate over raised structural flanges and deep channels with ease.
No. | Parameters |
Model | KD-MJQ-2 |
Max. Pressure | 25MPa |
Oil Pipe Length | 10000mm |
Oil Tank Capacity | 50L |
Gun Head Stroke | 50mm |
Iron Thickness | 1.5mm+1.5mm |
Power | 380VAC 50~60Hz 4.5kW |
Investing in the KD-MJQ-2 system extends far beyond immediate assembly improvements; it fundamentally reshapes the financial and operational dynamics of the production facility. The compact footprint of the main hydraulic unit, combined with the extended reach of the 10-meter umbilical, optimizes floor space utilization. Heavy busduct assemblies can remain stationary on the floor or assembly tables while the operator moves the clinching tool freely around the perimeter, drastically reducing material handling bottlenecks.


